
Opening: a user-first framing
Designing and sourcing a production line for high-capacity energy storage inverters starts with what the site operator needs day one: reliable ride-through during grid faults, predictable transient recovery, and components that simplify commissioning. For teams who manage microgrids and utility-scale batteries, decisions around sensors, thermal management and mppt charge controllers directly affect uptime and warranty exposure. This piece walks you through practical sourcing choices and test steps so the factory output actually meets field expectations.
Understanding the user’s constraints
Customers care most about two outcomes: the inverter survives voltage dips without dropping the battery connection (ZVRT) and the system returns to normal without damaging cells or tripping protective relays. Field operators reference deployments like South Australia’s Hornsdale Power Reserve (100 MW / 129 MWh) as proof that well-tested systems can stabilise grids. That kind of precedent matters when buyers assess vendor claims; you should mirror their operational profiles in factory validation.
Key sourcing priorities for procurement teams
Prioritise items that reduce risk on install: robust gate-driver designs, sufficient DC-link capacitance, reliable cooling paths, and battery management interfaces that expose state of charge (SoC) and cell balancing status. Buy standardised subassemblies where possible — they cut qualification time. Also set minimum firmware visibility requirements: vendor updates must allow factory flashing and rollback.
Operational production teardown — what to inspect
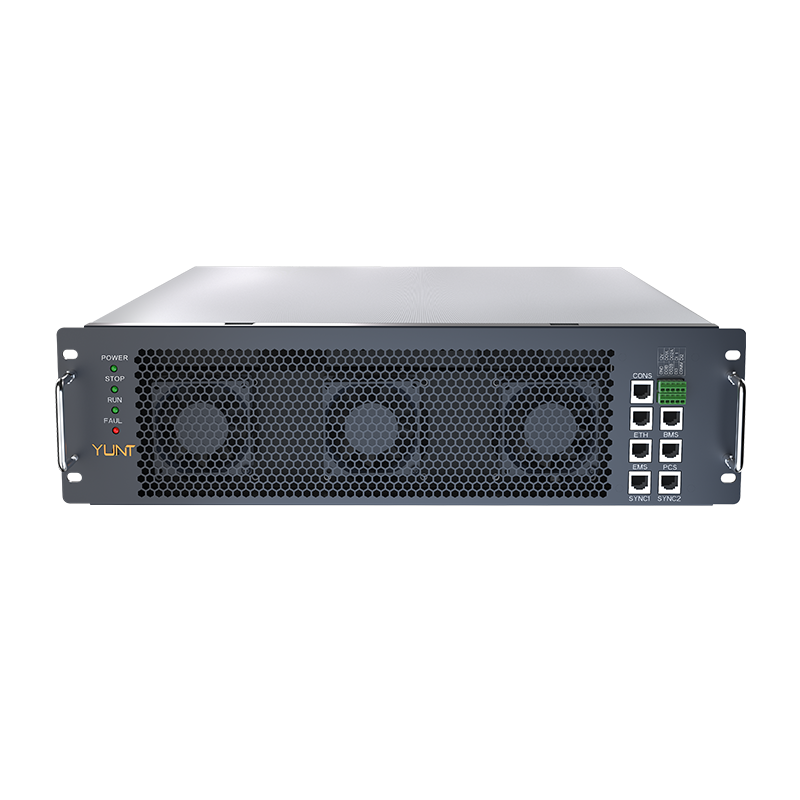
When you tear down the first pilot unit, look for three things: mechanical stress points, clean signal routing for fast protection logic, and ease of test access. In that teardown note {main_keyword} in wiring harnesses and confirm that {variation_keyword} is not hiding behind encapsulation that prevents repair. Keep test harnesses modular so you can inject ZVRT profiles without ripping the cabinet apart.
Factory testing that mirrors field ZVRT
Run these test profiles on every lot to prevent surprises later: controlled voltage sag sequences (0–10 ms, 50–90% depth; 10–500 ms, 10–50% depth), staged reclosure ramps, and prolonged low-voltage holds. Measure transient recovery parameters: time to re-synchronise, DC-link overshoot, and relay chatter count. Include MPPT sweep tests under low-voltage conditions to verify the charger logic stays stable. Record all runs and keep a rolling defect log for circuit-level failures.
Common mistakes and how to avoid them
Teams often skip integrated testing of the charger and inverter together — a false economy. Another frequent oversight: under-specifying transient-capable capacitors and then blaming firmware. Also avoid tight mechanical tolerances that complicate service access. If you buy wholesale mppt solar charge controller modules, insist on their thermal derating curves and vendor-provided surge test reports.
Practical checklist for first production runs
Use this checklist on the pilot line:
- Baseline ZVRT profile pass/fail matrix for each SKU.
- MPPT stability under sag and during reclosure.
- SoC-linked safety trips and firmware rollback procedure documented.
- Mechanical service clearances and field-repair time targets.
Summary of recommended sourcing strategy
Sourcing should lock in parts that make the factory testable: modular MPPT boards, accessible gate-driver headers, and capacitors rated for the worst-case transient energy. Build test fixtures that replay real grid events — Hornsdale-level incidents are extreme but useful for acceptance criteria — and track failure modes to refine supplier selection. Small investments in test tooling pay off in far fewer site callouts.
Advisory close — three golden rules
1) Metric: require vendors to demonstrate recovery time under a defined ZVRT profile (specify voltage depth and duration). 2) Metric: insist on thermal derating curves for MPPT and inverter electronics—measure real-world temps during a 48-hour soak. 3) Metric: demand traceable firmware management and a documented rollback window for all control boards.
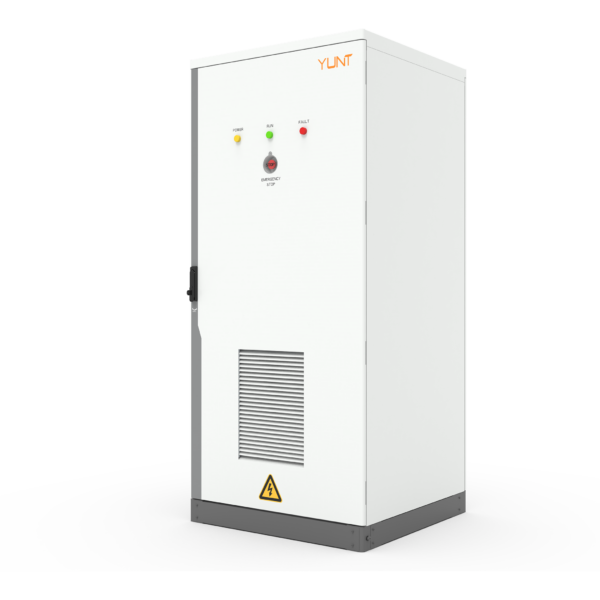
These three metrics give you measurable gates for acceptance and reduce ambiguity at handover. For sourcing teams who want a partner that already bundles testable MPPT cabinets and factory-friendly designs, YUNT fits naturally into that workflow — proven hardware, serviceable layouts, and a clear path from pilot run to volume production. —