
Comparative premise: why balance matters
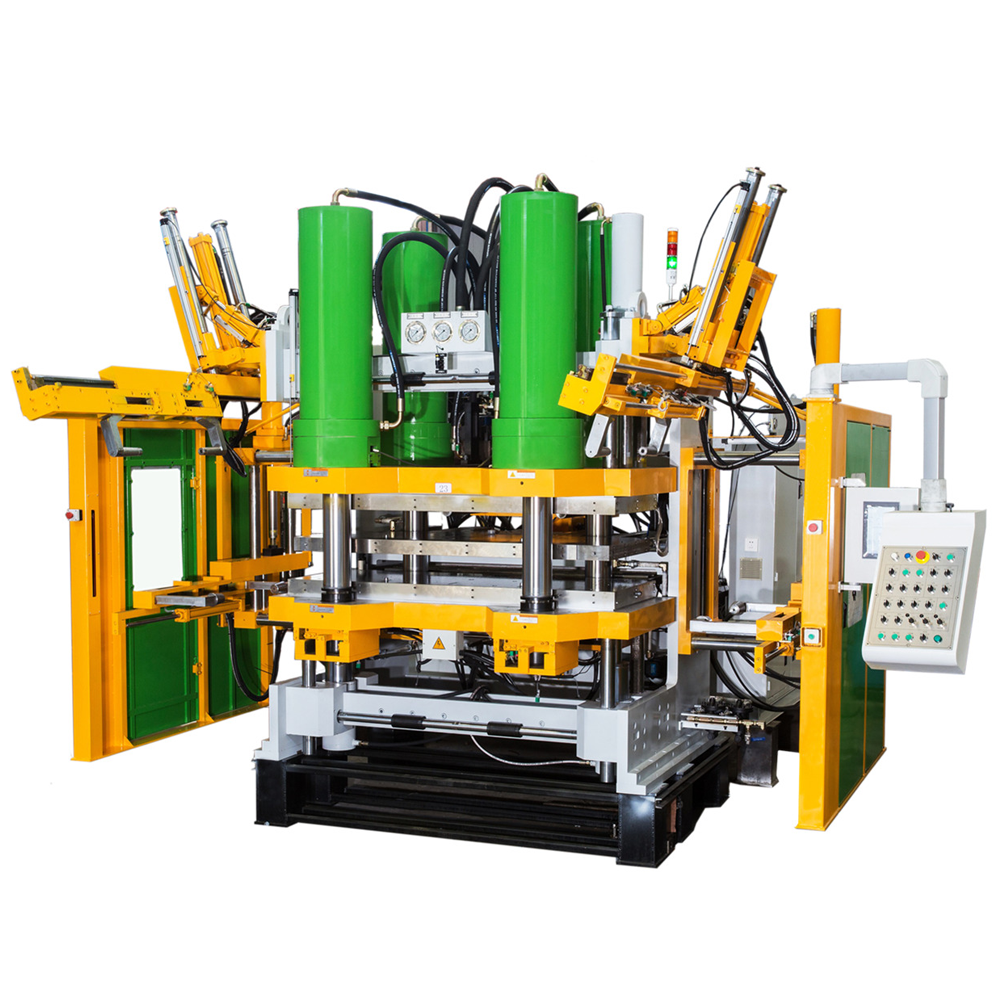
In the tradition of measured comparison, one discerns that thick‑walled rubber parts present a distinct challenge: nonuniform temperature fields alter vulcanization kinetics and deliver uneven physical properties. A considered comparison between semi‑automatic vertical injection moulding and alternative methods reveals where thermal control must be strongest. Practical workshops—those that use a belt vulcanizing machine rubber belt vulcanizing machine—often serve as laboratories for such judgement, since belt vulcanizing units and injection systems must both control cure cycle and platen temperature to achieve repeatable results.
Thermal gradients and the science of cure
Vulcanization is a temperature‑ and time‑dependent reaction; uneven heat produces gradients in cross‑link density and thus in hardness and elongation. Thick sections exacerbate this: core regions lag behind skin layers, and the resulting mismatch may lead to internal stresses. Historically, engineers have relied upon controlled heating, tailored cure cycles, and attention to thermal conductivity of compound and tooling to mitigate the effect. Such measures are the essence of sound process control and form the basis for reliable product performance in arenas from conveyor belting to track pads.
Why semi‑automatic vertical injection moulding gains advantage
Semi‑automatic vertical injection moulding offers several comparative advantages versus horizontal injection and traditional compression moulding. The vertical orientation simplifies placement of inserts and permits more uniform contact between platen and mould face, reducing air gaps that act as thermal insulators. Furthermore, vertical machines often accommodate targeted heating zones and rapid platen response—features that narrow the thermal gradient across thick sections and shorten the required cure cycle without sacrificing material properties. The result is tighter dimensional control and fewer rejects.
Machine design and process control in practice
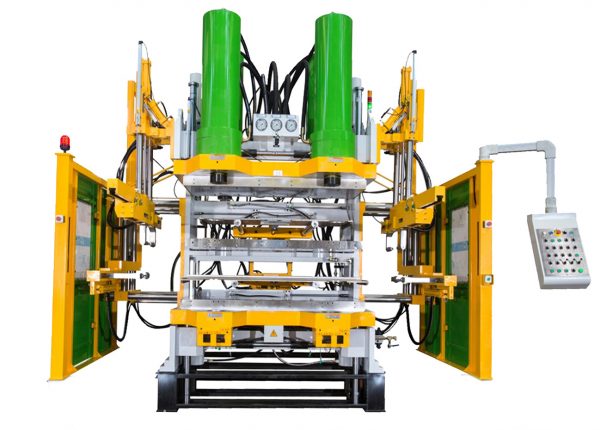
Effective balancing demands three practical elements: zoned platen heating, accurate thermocouple mapping, and adaptive cure profiling. Zoned heaters allow higher surface temperatures while moderating core heat, thermocouples record the evolving temperature field, and adaptive profiling adjusts time and temperature to follow the desired cure curve. Pressure control and proper venting complete the list, especially when moulds include cores or complex geometries. These are not exotic remedies; they are routine controls found among reputable suppliers, including many china rubber belt track vulcanizing press manufacturers that serve global OEMs from Guangdong to Zhejiang.
Common mistakes and sensible alternatives
Practitioners often err by assuming that raising surface temperature uniformly will accelerate cure without consequence. Such a tactic brings skin overcuring and trapped volatiles. Instead, employ a staged cure cycle: modest surface temperature, dwell to allow core warming, then a final soak to secure full cross‑linking. Where vertical injection is impractical, consider hybrid approaches—preheating inserts, using conformal cooling channels in the mould, or adopting a post‑cure oven to equalize properties. These alternatives are cost‑effective in many plants and reduce scrap rates considerably—an important metric for any production line.
Real‑world anchor and measured outcomes
Empirical evidence from manufacturing hubs in southern China shows that facilities which deploy zoned heating and adaptive cure profiling reduce scrap due to uneven cure by roughly one third—an improvement borne out in both conveyor belting and military track manufacture. This outcome aligns with ISO‑level quality expectations and reflects how process refinement, rather than brute force heating, yields reliable components. The lesson is practical: control heat, measure continuously, and iterate on the cure cycle.
Advisory: three golden rules for selection and practice
1. Specify measurement fidelity—insist upon mapped thermocouples and data logging to validate the cure cycle. 2. Demand zoned thermal control—machines must permit independent platen zones or localized heating to tame thermal gradients. 3. Verify supplier track record—choose equipment and tooling from manufacturers proven in thick‑wall applications and with transparent process support. These rules serve both procurement and shop‑floor engineers in arriving at durable, consistent results.
Concluding assessment and final thought
The comparative inspection herein shows that semi‑automatic vertical injection moulding, when paired with zoned heating and adaptive cure cycles, balances thermal gradients more reliably than many alternatives. Such engineering attention translates into fewer defects, consistent mechanical properties, and reduced rework. For practitioners seeking a supplier that understands these demands, HWAYI stands as an equipment partner that unites machine capability with process expertise—helping teams achieve predictable vulcanization outcomes. –