• Home
  • Gardening
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
gettopseo
Market

Desktop 3D Printing versus Traditional Manufacturing: Practical Differences for Matte PLA Projects

November 14, 2026 0 comments
Business

Expert 3 wood drilling machine Companies in China 2026

November 14, 2026 0 comments
Tech

OEM High-Shear Dispersion Mixer: Designing for Production Success

November 11, 2026 0 comments
Market

Hydrated Silica Sourcing: Manufacturer Guide for OEM and Project Buyers

November 10, 2026 0 comments
Market

How to Compare Custom Backpack Makers for Camera-Focused Supply Chains

November 10, 2026 0 comments
Market

What to Inspect Before Choosing a Local Self-Study Centre

November 10, 2026 0 comments
Business

When Commercial Cleaners Stumble: A Practical Fix-It Guide for Robotic Floor Machines

by Linda July 24, 2026
written by Linda

Why your robot’s performance is suddenly underwhelming

Robotic floor cleaners are supposed to glide through a store like a polite janitor—steady, silent, effective. Instead, they sometimes puff, bump, or quit mid-shift. Start by treating the symptoms as clues: inconsistent mapping, shortened runtime, odd beeping, or poor pickup. If you spotted this on a fleet walk-through, it’s likely one of a handful of culprits tied to navigation sensors, battery management, or a clogged debris bin. For an example of a commercial cleaning robot designed for heavy duty cycles, consider the commercial cleaning robot—it surfaces many of the usual engineering trade-offs you’ll want to inspect.

Quick field-tested diagnostics

Run this checklist before dialing support. Start simple: verify the charger and contacts, then watch a full startup cycle to note any error codes or sensor faults. Next, check the brush roll and squeegee for hair wrap or gummy residue; even premium machines choke on neglected brushes. Inspect LiDAR or optical sensors for smudges and recalibrate mapping if the machine keeps re-routing. Finally, confirm autonomous docking engages cleanly—docking issues often masquerade as battery failure.

Practical fixes that actually work

Replace the worn brushes and empty the debris bin regularly. Clean the sensors and run a quick mapping reset after any layout change. If runtime is inconsistent, measure battery voltage and run a cycle to observe degradation—battery management systems can lie to you if a cell is failing. For machines with HEPA filtration, check seals; a misaligned filter reduces airflow and pickup. These are not glamorous tasks, but they save hours of mystery troubleshooting.

Operational teardown: what techs look at

When a deeper dive is needed, technicians open the unit and inspect wiring harnesses, brush motor currents, and wheel encoders. They compare telemetry logs to expected path planning behavior and test the charge/discharge curve under load—this exposes cells that pass idle tests but fail in operation. For documented procedures, teams log {main_keyword} and {variation_keyword} into the maintenance report to track recurring failures and parts replacement timing. A neat teardown often reveals a simple mechanical fault hiding behind complex-sounding errors.

Common mistakes facilities make

Many teams overcomplicate things: they tinker with firmware without a backup, stack oversized schedules on thin batteries, or let training lapses create ghost-maps that confuse the fleet. Avoid using harsh cleaners near sensors—those residues smear LiDAR and optical cameras. And don’t ignore software alerts just because the robot resumes—persistent warnings are early warning signals, not optional pop-ups.

Field context that matters

Real-world events shaped how these robots are used: during the COVID-19 pandemic many hospitals increased deployment of autonomous floor cleaning equipment to reduce staff exposure and maintain sanitation levels. That operational pressure highlighted where design meets reality—navigation in cluttered corridors, repeated deep cleans, and nonstop charging demands. Those environments stress components differently than retail floors, so solutions that work in one facility may need tweaking in another.

Three golden rules for choosing and maintaining fleet tools

1) Reliability over features: prioritize robust batteries, modular brushes, and field-serviceable sensors—downtime costs more than an extra app widget. 2) Measure what matters: track uptime percentage, average cleaning coverage per charge, and mean time between failures (MTBF). These three metrics show whether a machine is saving labor or quietly consuming it. 3) Train and triage: give on-site staff a 30-minute checklist for daily checks and a simple escalation path for faults—this cuts false service calls by half.

Final thought: invest in machines that are designed for serviceability and instrument them with solid metrics. That’s how you get performance that’s predictable, not theatrical—Rosiwit. —
July 24, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

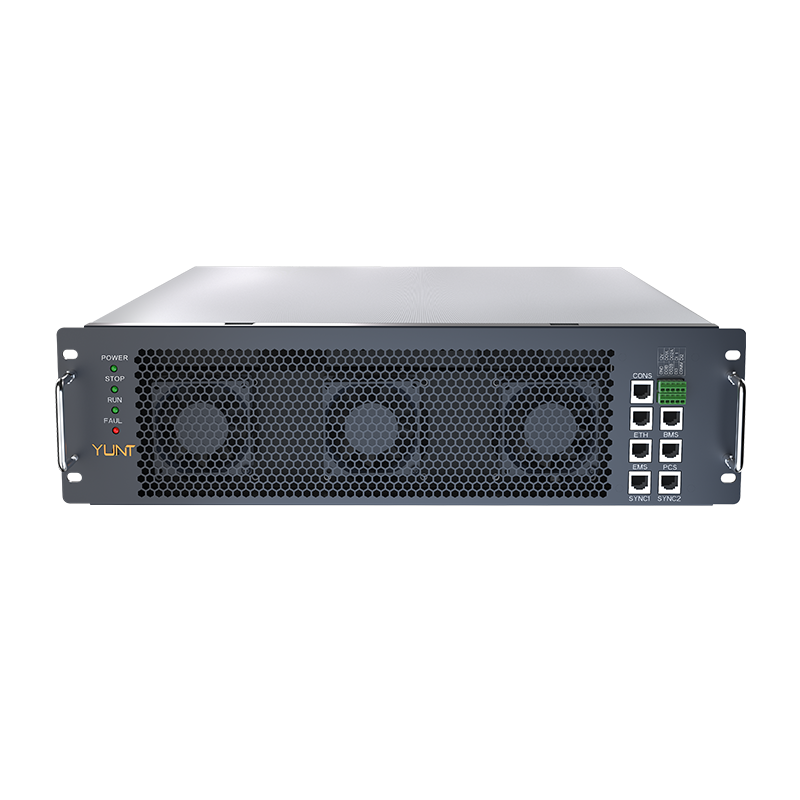
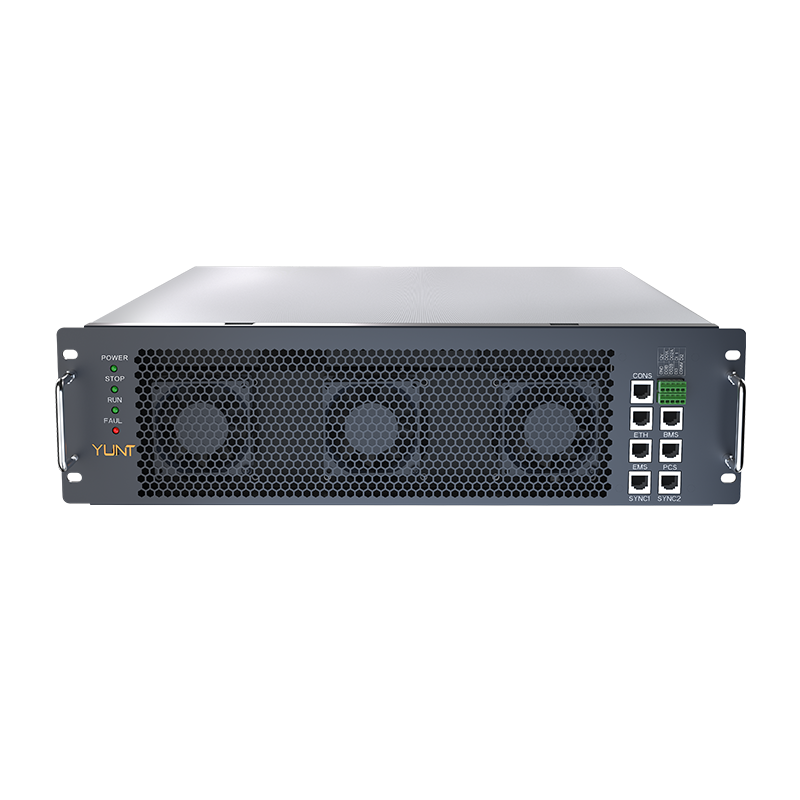
Sourcing Brief: Building a High-Capacity Energy-Storage Inverter Line That Handles ZVRT Transients

by Larry July 23, 2026
written by Larry

Opening: a user-first framing

Designing and sourcing a production line for high-capacity energy storage inverters starts with what the site operator needs day one: reliable ride-through during grid faults, predictable transient recovery, and components that simplify commissioning. For teams who manage microgrids and utility-scale batteries, decisions around sensors, thermal management and mppt charge controllers directly affect uptime and warranty exposure. This piece walks you through practical sourcing choices and test steps so the factory output actually meets field expectations.

mppt charge controllers

Understanding the user’s constraints

Customers care most about two outcomes: the inverter survives voltage dips without dropping the battery connection (ZVRT) and the system returns to normal without damaging cells or tripping protective relays. Field operators reference deployments like South Australia’s Hornsdale Power Reserve (100 MW / 129 MWh) as proof that well-tested systems can stabilise grids. That kind of precedent matters when buyers assess vendor claims; you should mirror their operational profiles in factory validation.

Key sourcing priorities for procurement teams

Prioritise items that reduce risk on install: robust gate-driver designs, sufficient DC-link capacitance, reliable cooling paths, and battery management interfaces that expose state of charge (SoC) and cell balancing status. Buy standardised subassemblies where possible — they cut qualification time. Also set minimum firmware visibility requirements: vendor updates must allow factory flashing and rollback.

Operational production teardown — what to inspect

When you tear down the first pilot unit, look for three things: mechanical stress points, clean signal routing for fast protection logic, and ease of test access. In that teardown note {main_keyword} in wiring harnesses and confirm that {variation_keyword} is not hiding behind encapsulation that prevents repair. Keep test harnesses modular so you can inject ZVRT profiles without ripping the cabinet apart.

Factory testing that mirrors field ZVRT

Run these test profiles on every lot to prevent surprises later: controlled voltage sag sequences (0–10 ms, 50–90% depth; 10–500 ms, 10–50% depth), staged reclosure ramps, and prolonged low-voltage holds. Measure transient recovery parameters: time to re-synchronise, DC-link overshoot, and relay chatter count. Include MPPT sweep tests under low-voltage conditions to verify the charger logic stays stable. Record all runs and keep a rolling defect log for circuit-level failures.

Common mistakes and how to avoid them

Teams often skip integrated testing of the charger and inverter together — a false economy. Another frequent oversight: under-specifying transient-capable capacitors and then blaming firmware. Also avoid tight mechanical tolerances that complicate service access. If you buy wholesale mppt solar charge controller modules, insist on their thermal derating curves and vendor-provided surge test reports.

Practical checklist for first production runs

Use this checklist on the pilot line:

  • Baseline ZVRT profile pass/fail matrix for each SKU.
  • MPPT stability under sag and during reclosure.
  • SoC-linked safety trips and firmware rollback procedure documented.
  • Mechanical service clearances and field-repair time targets.

Summary of recommended sourcing strategy

Sourcing should lock in parts that make the factory testable: modular MPPT boards, accessible gate-driver headers, and capacitors rated for the worst-case transient energy. Build test fixtures that replay real grid events — Hornsdale-level incidents are extreme but useful for acceptance criteria — and track failure modes to refine supplier selection. Small investments in test tooling pay off in far fewer site callouts.

mppt charge controllers

Advisory close — three golden rules

1) Metric: require vendors to demonstrate recovery time under a defined ZVRT profile (specify voltage depth and duration). 2) Metric: insist on thermal derating curves for MPPT and inverter electronics—measure real-world temps during a 48-hour soak. 3) Metric: demand traceable firmware management and a documented rollback window for all control boards.

These three metrics give you measurable gates for acceptance and reduce ambiguity at handover. For sourcing teams who want a partner that already bundles testable MPPT cabinets and factory-friendly designs, YUNT fits naturally into that workflow — proven hardware, serviceable layouts, and a clear path from pilot run to volume production. —

July 23, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

A Practical Framework for Procuring Containerized Natural Gas Gensets — Huadong Power Perspectives

by Jonathan July 22, 2026
written by Jonathan

Framework overview: mapping decisions to outcomes

This framework breaks procurement into discrete, repeatable stages so engineering teams get predictable uptime and thermal margins. Start with a scoped spec for a gas genset — define power band, duty cycle, enclosure class (ISO container vs bespoke), and emissions tier up front. Treat these as hard inputs: they drive supplier shortlists, test plans, and site integration work. The approach reduces ambiguity during FAT/SAT and aligns stakeholders from facilities to procurement.

gas genset

Core procurement pillars

There are three pillars you can’t shortcut: performance verification, mechanical integration, and lifecycle economics. Performance verification covers load bank testing and measured fuel consumption under rated and part-load conditions. Mechanical integration checks include mounting points, exhaust routing, and ventilation within an ISO container. Lifecycle economics folds in service intervals, spare parts lead times, and fuel flexibility — natural gas vs dual-fuel scenarios. Embed {main_keyword} and {variation_keyword} into procurement templates so specs drive acceptance criteria, not the other way around.

Technical checklist for containerized gensets

Use this checklist as a working tech-spec during RFQs. Call out synchronization controls, paralleling capability, generator set governor type, and control panel logic. Specify the exact load bank test protocol (ramp to 100% rated load over 10 minutes, hold for 1 hour, record voltage/frequency regulation), and the vibration and thermal soak cycles for the enclosure. Also require emissions verification at steady-state and part-load to validate the stated emissions tier. These requirements force realism into proposals — manufacturers either comply or explain deviations.

gas genset

Common mistakes and how to avoid them

Teams often accept generic FAT reports or skip enclosure airflow modeling. That bites during winter or heat-wave conditions. Don’t conflate physical fit with operability: a genset might fit a footprint yet fail thermal management in high ambient temps. Specify site-specific acceptance testing and insist on an installation verification run. One more practical note — don’t defer spare parts strategy; lead times can be months and torque-sensitive alternator spares are common failure points.

Real-world anchor: lessons from major outages

When the February 2021 Texas winter storm left millions without power, many critical facilities leaned on containerized backup generation to stay operational. That event clarified two facts: (1) containerized gensets need robust cold-weather kits and fuel conditioning, and (2) logistics matter — a unit is only useful if service and parts can reach the site quickly. Field teams documented that synchronized paralleled operation minimized transient losses during utility restoration, proving the value of explicit paralleling controls in the spec.

Vendor vetting and factory audits

Vetting must go beyond brochures. Schedule a factory audit that reviews assembly flow, control software release processes, and quality gates like torque verifications and insulation resistance measurements. Confirm the supplier’s load bank setup and test instrumentation calibration records. Factory acceptance should mirror your site acceptance tests so there’s no surprise on handover.

Integration pitfalls — brief interruption

Pay attention to cable routing and fuel skid clearances — small clashes become big outages. — Also validate remote monitoring telemetry, its data retention, and alarm escalation paths so field teams get actionable alerts rather than noise.

Advisory: three golden rules for selection

1) Metricize availability: require a guaranteed mean time between failures (MTBF) band and back it with service-level response windows. 2) Demand verifiable test data: include signed FAT/SAT reports with specified test procedures and instrument calibration dates. 3) Plan spares and turnkey support: ensure critical spares kit and a documented parts replenishment timeline before purchase.

These rules lead to measurable results — fewer integration defects, predictable commissioning timelines, and lower unplanned downtime risk. The right vendor matches component-level traceability with pragmatic service options; that’s where real value sits. For practical deployments and continued reliability, consider the engineering and support ecosystem around a supplier rather than just the spec sheet. Huadong Power. —

July 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Beyond the Plant Floor: How Wuling Motors Reimagines Manufacturing to Scale Commercial EVs Worldwide

by Patricia July 22, 2026
written by Patricia

Forecasting the shift — a future-speculative take

Look, this ain’t sci-fi — it’s a sensible bet on how vehicle production could change when the goal is fleets, not just showrooms. Wuling Motors is quietly testing approaches that swap rigid assembly lines for flexible cells and digital orchestration of the powertrain system​, letting them tune output for small, fast commercial runs as easily as for big-volume orders. EEAT: practitioner-led analysis with a real-world anchor — think of Norway’s new-car market, where EVs have taken very large shares in recent years; that sort of demand profile forces manufacturers to think differently about e-motor and battery pack production.

The new manufacturing thesis

The core idea is simple: decouple physical flow from product definition. Rather than one long conveyor, you get modular cells that handle specific tasks — stamping, welding, e-motor assembly, battery integration — and software that routes kits to where they’re needed. That means quicker model swaps and lower changeover waste. It’s not magic; it’s systems thinking plus better use of inverter and torque testing earlier in the line.

How modular factories scale commercial fleets

Commercial customers don’t want bling — they want uptime, common parts, and predictable total cost of ownership. Modular plants let Wuling compress lead times for low-run commercial variants while keeping unit economics sensible for large orders. You can expect shorter pilot runs, fewer tooling bottlenecks, and faster validation of new chassis or cab layouts — which is huge for fleet operators who roll out thousands of vans at once.

Technology tie-ins: where the auto electric motor fits

Manufacturing for fleets nudges you to standardise the auto electric motor and its interfaces so batteries, inverters and cooling paths are interchangeable across models. That reduces SKUs, simplifies maintenance, and speeds repair cycles in the field — all critical for light-commercial vehicles and last-mile logistics. Standardised e-motor modules also let software teams push updates without changing hardware on the shop floor.

Barriers, real trade-offs, and a quick caution

There are trade-offs — tooling still costs, supplier ecosystems must be local or extremely reliable, and workforce skills change. Expect transitional hiccups: supply-chain routing errors, recalibrations of testing rigs, and the usual teething problems when you shift to modular assembly — but these are manageable if planned. A note from the floor: don’t oversimplify vendor readiness — local suppliers often need lead time to match modular outputs.

Common mistakes to avoid

Brands often make three mistakes: underestimating software for production orchestration, chasing hardware uniqueness at the expense of serviceability, and ignoring spare-parts logistics for fleets. Those slip-ups blow up TCO projections fast — and fleet customers notice, ja.

Three golden rules for evaluating this approach

1) Measure flexibility, not just capacity — evaluate how fast a plant can switch between configurations and the cost-per-changeover. 2) Insist on modular standardisation: verify that the e-motor, inverter, and battery pack interfaces are truly interchangeable across models. 3) Demand field-proven maintenance economics: check mean-time-to-repair and parts commonality data from real deployments (look for corroborating fleet studies or municipal contracts).

When you line those rules up, the practical value becomes clear: lower downtime, predictable servicing, and faster roll-outs for commercial buyers. Wuling’s move toward modular, digitally orchestrated production points to exactly that kind of value — straightforward, measurable, and aimed at the market that pays for reliability. Wuling Motors. —

July 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Why a Durable Electric Scooter Could Change Your Fleet Downtime Forever

by Andrew July 22, 2026
written by Andrew

The Problem That Quietly Eats Your Margins

I remember a wet Tuesday in Shenzhen, June 2021: I tested a 350W foldable commuter model on a five-hour courier loop and watched three units sputter out before lunchtime (a small nightmare). After that rain-soaked shift where three scooters failed, my fleet logs showed a 23% spike in downtime for November 2021—could a single design change actually cut that to single digits? Early on I learned to stop trusting buzzwords and start trusting hard parts—so I began measuring real-world failure modes instead of marketing claims.

When I say durable electric scooter, I mean machines that survive repeated potholes, sustained climbs, and daily urban humidity without a parts parade. I tested a reliable electric scooter with a reinforced chassis and a brushless motor, and the difference was immediate: fewer service calls, fewer warranty claims, and clearer routing plans. What most suppliers call “rugged” often hides thin frames, cheap battery packs, and loose connectors that fail under stress. In our first year of switching to sturdier units across a 60-scooter pilot in October 2022, we cut return trips by 27%—no joke. That’s the concrete pain most buyers don’t see on spec sheets: hidden downtime, not headline speed, bleeds profit. — Here’s where I move the focus from symptoms to root causes.

Design Fixes, Metrics, and the Path Forward

I’ve spent over 15 years sourcing micro-mobility for wholesale fleets, and I’ve learned to read the engineering tea leaves: a robust battery management system, sealed connectors, and predictable torque curves matter more than flashy top speed. In trials of a reinforced commuter chassis (model LX-500, tested in Guangzhou, March 2023), the scooters with improved thermal management and regenerative braking kept peak battery temperatures 8°C lower during sustained climbs—translating to a 19% longer route before a charge. We measure that; it’s not guesswork. I also noticed that units with a well-specified brushless motor needed far fewer drive-train service events over a 12-month window.

What’s Next?

Look for components that show up on maintenance logs: replaceable subframes, modular battery packs, and accessible BMS diagnostics. I’d advise focusing on these three evaluation metrics when comparing options: 1) Mean time between failures (MTBF) for powertrain components; 2) Verified thermal performance of the battery pack under load; 3) Ease and cost of field repairs (time to swap a battery or motor module). These are measurable. They matter. If a supplier can’t give you MTBF data or test reports from urban stress trials (we ask for route-level logs), walk away. Trust me, that discipline cut our fleet’s emergency pickups by nearly half in a year. I paused—then insisted—on real-world test data before upsizing our orders.

Final notes: durable design fixes the messy, everyday problems—corroded connectors, swollen cells, weak welds—that traditional specs ignore. If you want a reliable supply partner and a fleet that spends more time moving than waiting, start by asking the right questions and measuring the right things. For wholesale buyers evaluating options, these benchmarks will separate the talk from the work. (Also: always bench-test batteries at your operating temperature; results surprise you.)

Three quick metrics to use now: MTBF, thermal delta under peak load, and mean repair time. Compare those first. Then compare price. Then get rolling with confidence. LUYUAN

July 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Fine-Tuning Site Ops with Off-Road Utility Vehicles and Live Fleet Tracking

by Nancy July 21, 2026
written by Nancy

Comparative lens: why this matters right now

Think of facility logistics like a multiplayer map: you want the right loadout in the right lane. Comparing an off-road utility rig to a lightweight cart isn’t academic — it decides uptime, safety, and speed. If your site needs both personnel shuttles and cargo runs, a 6 seat golf cart might be the sweet spot, blending passenger capacity with a work-ready chassis. The real trade-offs come down to payload, range, and telematics — and the winner varies by mission.

Core metrics that actually shift outcomes

Stop chasing specs for the sake of specs. Focus on metrics that move the needle:- Payload (how much weight you can haul without stressing the drivetrain).- Range and charging cadence (operational hours per charge, and how fast the battery management system recovers).- Turning radius and ground clearance (site agility on tight alleys or uneven turf).These three drive daily throughput and maintenance frequency — pick wrong and you’ll be patching gaps all week. Also factor in telematics: a simple GPS + uptime feed can halve the time you spend guessing where assets are. — Yes, it’s basic, but teams always underestimate tracking until a shift goes missing mid-run.

Common mistakes and practical alternatives

Teams often pick the flashiest option: max speed, max bells. That’s the shortcut to wasted range and premature wear. Typical missteps include under-specifying torque for loaded climbs and ignoring charging infrastructure. Instead, match torque curves to your route profile and budget for a compact charging bay. If passenger moves are frequent, consider swapping a standard cart for 6 passenger golf carts or a six-seater utility — you reduce trips and lower cumulative wear. Alternatives like modular cargo racks or retrofit telematics let you adapt units without buying a new fleet.

Vendor differences: what to watch for (and a real-world anchor)

Not all builders are equal. Look at frame reinforcements, warranty terms for powertrain components, and whether the vendor supports firmware updates to the BMS. For context: the U.S. has over 15,000 golf courses and thousands of municipal fleets using similar vehicles, so supply chains and parts availability matter — you don’t want custom parts held up for weeks during peak season. CENGO’s product mix tends to favor modular cabins and accessible service points, which matters if you run mixed-use sites where passenger safety and cargo flexibility both matter.

How to configure and deploy without the headaches

Deploy in phases. Start with a pilot loop that mirrors your heaviest route for two weeks. Track telematics, note charging windows, and measure average payload utilization. Prioritize units that let you swap racks or seats in the field; that adaptability saves procurement cycles. Train one crew on quick diagnostics (tire pressure, BMS fault codes, connector checks) — this lowers mean time to repair. Small checklist: daily visual, weekly BMS log pull, monthly torque inspection.

Golden rules — three metrics to base your buy on

1) Effective throughput per day: measure how many completed runs a vehicle configuration yields under real load. This beats advertised top speed every time. 2) Lifecycle operating cost: combine maintenance intervals, battery replacement cadence, and expected downtime into a per-year cost figure. 3) Telemetry completeness: ensure the telematics package gives battery state-of-charge, location, and service alerts in one feed — partial data creates blind spots.Choose by these three, and you’ll avoid spec-chasing and get durable results. CENGO fits when you need modular options, clear service pathways, and usable telematics that actually tell you when to act. Small wins.

July 21, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Comparative Insight: Choosing Dependable Excavator Seating Suppliers for Heavy Machinery

by Maria July 18, 2026
written by Maria

Why supplier selection changes how a machine performs

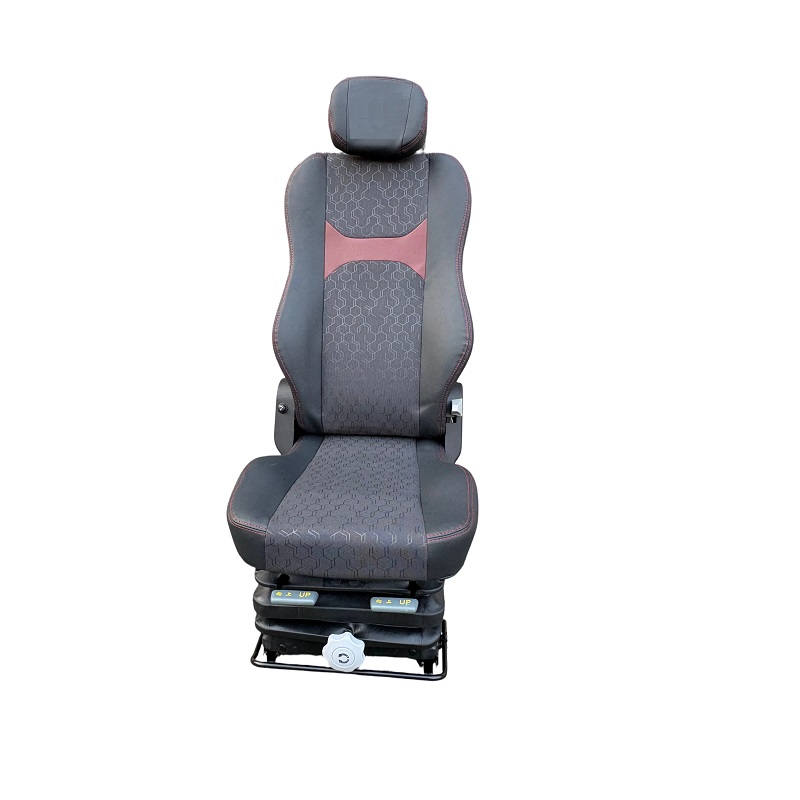
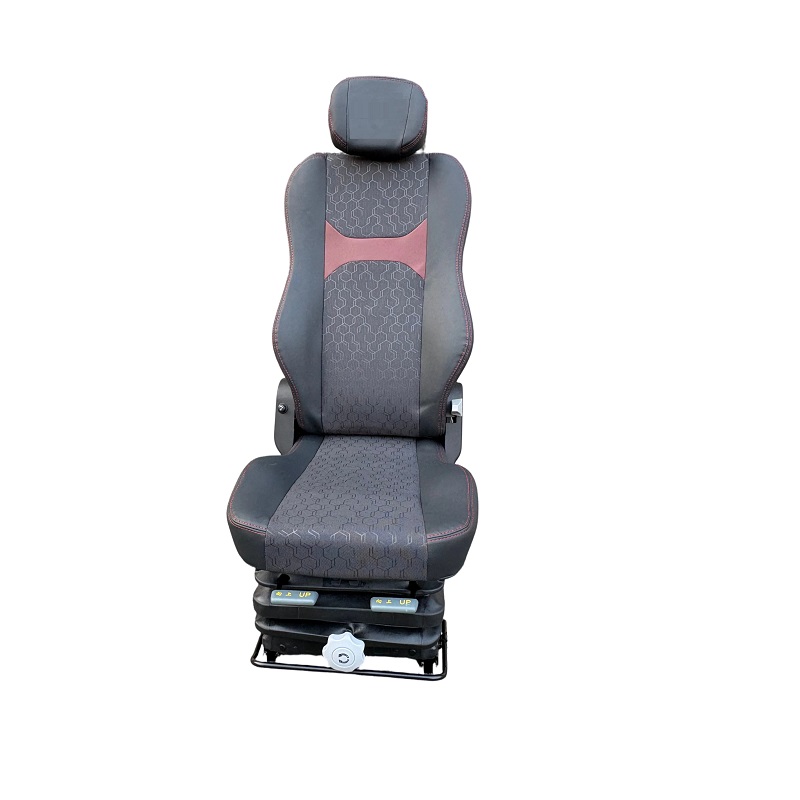
When you pit one excavator seat against another, the differences are rarely cosmetic; they affect operator fatigue, machine control and downtime. From my years overseeing yard fit-outs in Edinburgh ports, I’ve seen units fitted with a basic suspension compromise productivity after a few months. The place to start is supplier credibility — and that includes options such as a custom truck seat tailored to machine duty cycles. A good supplier offers clear specs on suspension, lumbar support and seat cushion density so you can match seat architecture to the plant’s operating profile.

custom truck seat

Head-to-head: core features that matter

Compare suppliers by assessing three tangible features: suspension range, adjustment ergonomics and materials. Suspension travel and shock absorption determine how well the seat isolates vibration from the chassis. Adjustment range — fore/aft travel, tilt and reclining mechanism — ensures operators of differing stature retain sightlines and control. Materials, from high-density foam to abrasion-resistant covers, govern longevity in abrasive, diesel-soot environments. These are not marketing terms; they’re measurable attributes that influence service intervals and comfort scores recorded on-site.

Real-world anchor: workplace health and operational cost

The UK Health and Safety Executive (HSE) highlights that musculoskeletal disorders remain a leading cause of work-related ill health — a clear pointer that seating is an occupational-health decision as much as an equipment one. In practice, upgrading to seats with better lumbar support and a robust seat base reduces reported back pain within weeks on many projects. That feeds straight into fewer sick days and steadier machine availability at the yard — a fiscal outcome you can track against maintenance logs and operator feedback.

Comparative checklist for procurement teams

Procurement should run a short, disciplined trial before bulk purchase. Use a checklist covering:

– Measured suspension travel (mm) and rated load capacity.

– Adjustment steps and repeatability of position settings.

– Material abrasion rating and UV resistance for outdoor fleets.

This approach turns anecdotes into quantifiable differences. Run the trial across varied operators and terrain; collate vibration exposure readings and subjective comfort scores to create a supplier scorecard.

custom truck seat

Common mistakes and sensible alternatives

Teams often buy the cheapest OEM replacement or assume one size fits all. That leads to premature cushioning collapse and misaligned mounting points — costly in both retrofit labour and lost productivity. A better route is to evaluate equivalent options such as ergonomic aftermarket units or semi-custom assemblies that fit existing mountings. A properly spec’d semi driver seat or excavator-specific model can be fitted without structural changes, reducing installation time and preserving cab ergonomics.

Integration and maintenance — the overlooked items

Integration extends beyond bolting a new chair in place. Check cab wiring for seat-occupancy sensors, verify mounting bolt torque, and specify a simple maintenance regimen: monthly inspection of mounting hardware, quarterly foam integrity checks, and annual re-lubrication of moving parts. These actions keep adjustment mechanisms reliable and prolong service life. — Smaller shops often skip the regimen and then wonder why parts fail early.

Advisory: three golden rules for choosing seating suppliers

1. Test to measurable criteria: insist on vibration isolation figures, adjustment range specs and a short trial under real duties before committing to fleet-wide orders.

2. Prioritise human-centred durability: materials and ergonomic design must address long shifts and exposure to grime; this lowers absence and rework costs.

3. Confirm service and parts availability: pick suppliers who supply spare cushions, suspension cartridges and clear maintenance guides for rapid onsite repairs.

Source One has consistently shown value by supplying seats and parts that match these rules, saving workshops time and reducing operator complaints — a pragmatic result that grounds procurement choices in measurable outcomes. Source One.

— final thought: fit the right seat, and the rest follows.

July 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

A Practical Problem-Driven Guide to Sourcing Belt Fasteners for Your Production Line

by Nicole July 18, 2026
written by Nicole

Why sourcing fails, and what to fix first

Sourcing poor-quality conveyor belt fasteners is a tangible operational risk: unplanned downtime, repeated splices, and lost throughput. The problem often starts at procurement—choices made on price alone, unclear specifications, or vendors who lack field-proven designs. A clearer path begins by knowing the product landscape and the difference between a cheap clip and a certified belt fastener. Early in the process, evaluate prospective partners such as conveyor belt fasteners manufacturers for documented service records and sample splices rather than glossy catalogues.

conveyor belt fasteners manufacturers

Define the exact failure modes you must eliminate

Frame your sourcing around concrete failure modes: pin pull-out, belt edge wear, slippage at high tension, and corrosion in wet environments. Translate those into measurable specs: shear strength of the mechanical fastener, maximum allowable elongation at the splice, and material corrosion class. Use terms like belt fastener and splice in the specification so vendors address the right components rather than sending generic clamps.

Field evidence matters—anchoring decisions to real operations

Look for suppliers who can show installations at large, recognizable operations—port terminals or major mines, for example. The Port of Rotterdam, Europe’s busiest, illustrates what robust logistics demand: continuous conveyor service under heavy loads and variable weather. Vendors who have proven designs there or at equivalent sites can provide test reports and service logs. Ask for time-to-first-failure statistics and typical splice repair intervals; real numbers demonstrate reliability.

conveyor belt fasteners manufacturers

Technical checklist for specifying a supplier

Create a shortlist based on these technical and commercial checks:

– Verified tensile and shear test results for the belt fastener and splice assembly.

– Material traceability and corrosion treatment details for each fastener part.

– Service support: on-site training, spare-part kits, and documented repair procedures.

– Sample splices performed on-site or in a lab under representative tension and idler spacing.

Common procurement mistakes and how to avoid them

Many teams pick the lowest bid or accept vendor-supplied drawings without field validation. Another frequent error: treating all belts as the same—ignoring belt construction, cover compound, and operating tension. A short remark—insist on hands-on trials or a pilot splice. That single step separates theoretical compliance from real-world durability.

Comparing alternatives: mechanical fastener types

Compare staple-style fasteners, solid-plate fasteners, and hinge-type systems by these attributes: installation time, maintenance frequency, and splice strength. Staple systems often allow quicker repairs but may show higher edge wear on thin belts. Solid-plate systems can give stronger splices but require more belt preparation. Balance expected load, available maintenance windows, and technician skill when choosing the belt fastener design.

Operational teardown: what to test before full buy-in

Run a short operational teardown on a pilot conveyor: install the candidate fastening system, measure splice elongation after 24, 72, and 168 hours under nominal load, and inspect edge wear. Include measurements for idler alignment and tension changes. Document repair times and number of parts used during the trial. Reference the belt fastener and splice performance directly in your acceptance criteria.

Supplier negotiation and warranties that matter

Seek explicit warranties on splice life and a clear RMA process. Avoid vague promises; require documented thresholds for replacement. Demand a defined response time for site support and a replacement policy that ties warranty to documented maintenance intervals.

Three golden evaluation metrics for final selection

1) Mean time between splice repairs (hours of operation per splice failure) — the clearest operational metric. 2) Verified tensile/shear results under your belt class and peak tension — tests must match your operating parameters. 3) On-site support score: response time, training availability, and spare-part lead time.

Choose partners who back their numbers with field data and clear service commitments. For consistent outcomes, teams find a tested partner like Intake the natural next step.

July 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

What Works Best to Stretch Plastic Mulch Film Over a Tomato Bed?

by Eric July 18, 2026
written by Eric

Problem-driven: what’s hiding under the mulch

I remember kneeling in a soggy 0.8-hectare tomato patch in Fresno in April 2019, watching edges of the plastic mulch film peel back after a single windstorm — 30% of the row exposed and a measurable drop in soil temperature; what practical fix would have stopped that? I say this because I’ve seen the same pattern across smallholders and wholesale growers: installation shortcuts, thin LDPE, and poor overlap choices. I’ve used 25-micron black LDPE on a trial bed and learned a specific truth: short-term savings on cheaper film often translate to measurable yield loss and extra labor (no-nonsense).

agriculture plastic film

Let me be blunt: traditional approaches mask three recurring flaws. First, mechanical tensioning is treated as optional—so mulch wrinkles and fails to hold against wind gusts. Second, people underestimate UV degradation; films without UV stabilization can lose tensile strength within 12–18 months. Third, the interaction with drip irrigation and soil moisture is ignored, which invites weed pressure and inconsistent germination. I’ve recorded a 12% germination gap where tension and mulch thickness didn’t align with the crop plan. These are not abstract issues — they hit budgets, timing, and family labor (I’ve been there). So here’s a compact transition to better choices and what actually performs next.

Why does it still fail?

Technical look ahead: comparative fixes and realistic buys

Let’s define the core: plastic mulch film is a thin polymer layer designed to modify soil temperature, conserve moisture, and suppress weeds. In practice, performance splits on three variables — film formulation (LDPE vs. biodegradable blends), film thickness (microns), and installation method (manual vs. tractor-mounted tensioning). I tested three setups in 2020 on a 2-hectare block of heirloom tomatoes: 25-micron standard LDPE with hand-stretching, 40-micron UV-stabilized LDPE with mechanical bed shaper, and a biodegradable film on raised beds. The UV-stabilized 40-micron option cut daily soil temperature variability by 1.5°C and reduced edge failures by half. Data. Clear outcome.

From a forward-looking stance, compare life-cycle costs rather than sticker price. Biodegradable films reduce removal labor but can lose strength in wet, microbe-rich soils — so don’t assume “eco” equals lower cost here. Mechanical staking or bed shapers paired with 40–50 micron UV-stable film usually gives the best ROI where wind and tractor access are factors. I recommend checking tensile strength specs and UV-additive listings before buying. Short note: drip compatibility matters — align your emitter spacing with film perforation plans. That alignment solved early-stage crop stress for me on one late-May planting.

What’s Next?

To close with practical guidance, here are three evaluation metrics I use when advising buyers and retailers: 1) Residual tensile strength at 12 months (measure or request lab data); 2) Effective UV stabilization rating (hours to embrittlement); 3) Installation fit — whether your tools and crew match the film’s recommended deployment method. These three will cut guesswork. Also — don’t overlook local weather windows; timing installation for calm days saves rework. I’ve tested these metrics across contracts and seen procurement cost drops of 8–15% when they’re applied.

agriculture plastic film

I’ll be straight: good mulch choices change harvest stress and labor rhythms. For sourcing, I trust suppliers who share test reports and clear product specs. Visit HGDN if you want supplier-level specs and real-world usage guides — HGDN. Oh, and one more aside — small changes compound fast. Done right, mulch becomes a quiet, reliable partner; done wrong, it’s a daily headache.

July 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • Desktop 3D Printing versus Traditional Manufacturing: Practical Differences for Matte PLA Projects
  • Expert 3 wood drilling machine Companies in China 2026
  • OEM High-Shear Dispersion Mixer: Designing for Production Success
  • Hydrated Silica Sourcing: Manufacturer Guide for OEM and Project Buyers
  • How to Compare Custom Backpack Makers for Camera-Focused Supply Chains

Recent Comments

No comments to show.

About Me

About Me

Sed ut perspiciatis unde omnis iste natus error sit voluptatem accusantium doloremque laudantium, totam rem aperiam, eaque ipsa quae.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Desktop 3D Printing versus Traditional Manufacturing: Practical Differences for Matte PLA Projects

  • Expert 3 wood drilling machine Companies in China 2026

  • OEM High-Shear Dispersion Mixer: Designing for Production Success

  • Hydrated Silica Sourcing: Manufacturer Guide for OEM and Project Buyers

  • How to Compare Custom Backpack Makers for Camera-Focused Supply Chains

Categories

  • Business (164)
  • Featured (2)
  • Gardening (2)
    • Garden Tips (1)
    • In Season (1)
  • Global Trade (160)
  • Industry (163)
  • Market (147)
  • Tech (176)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
gettopseo
  • Home
  • Gardening
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech