
Introduction: The System Behind the Shine
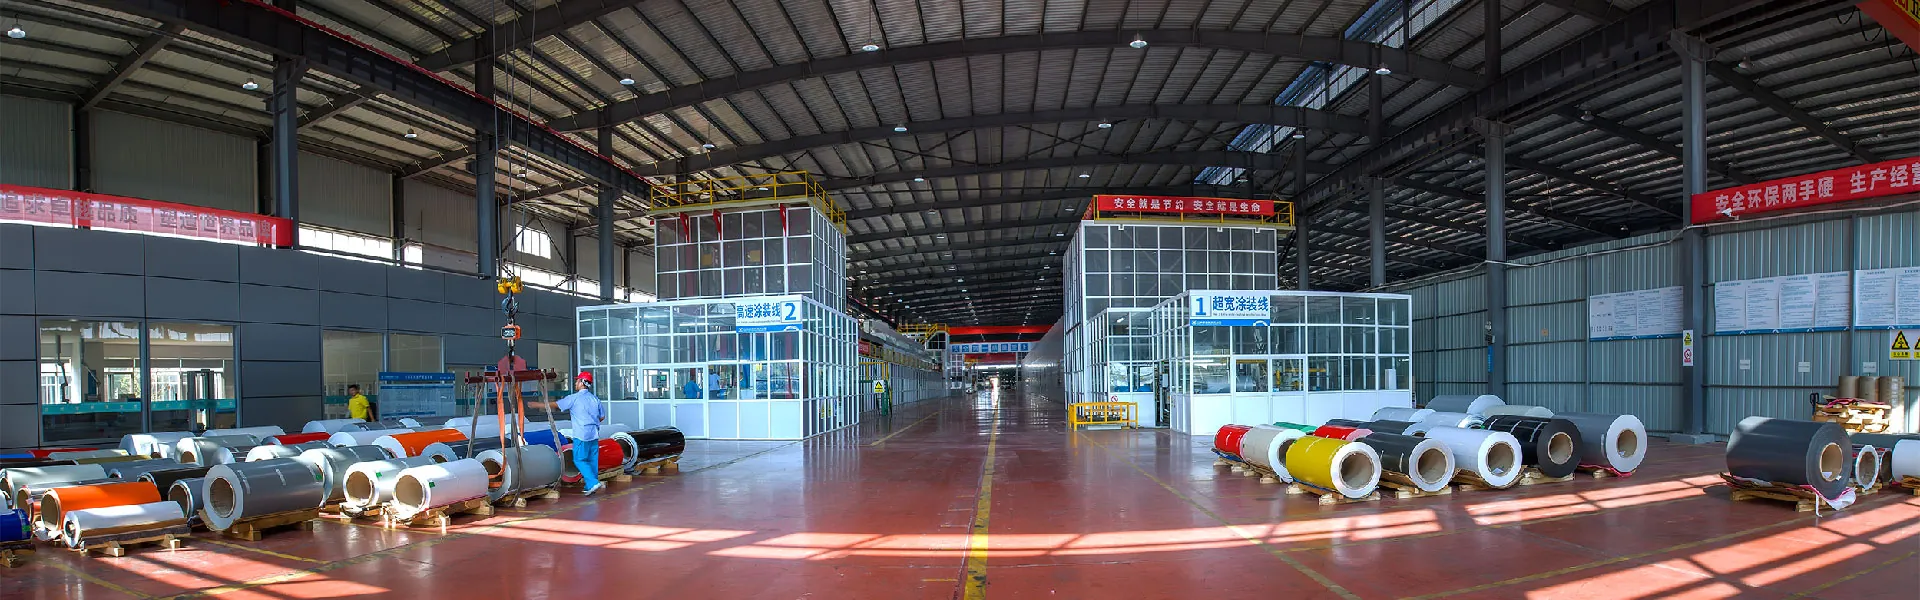
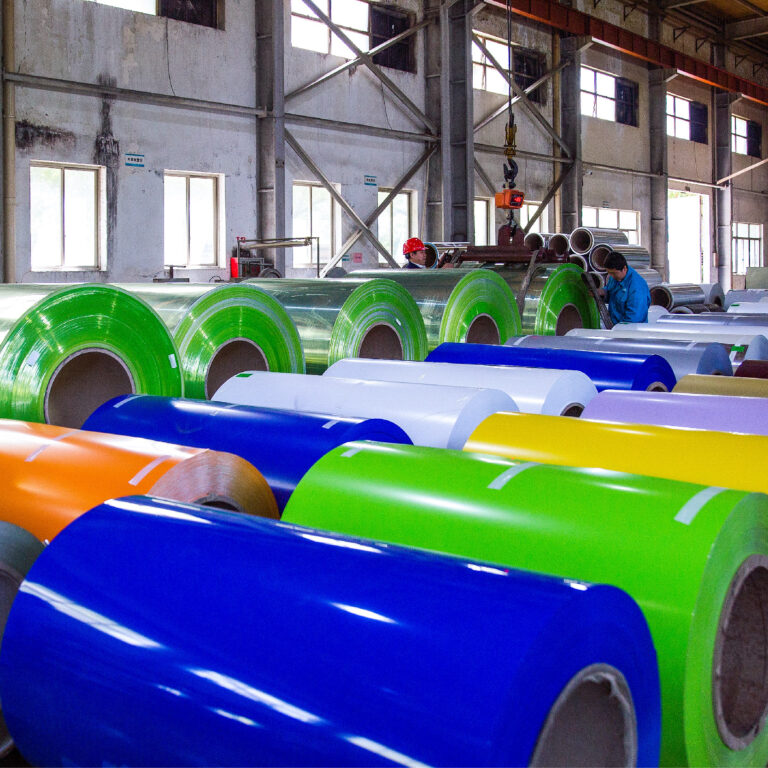
Technical first. Coil coating is a continuous process. It locks performance into metal before you even cut a panel. Painted Aluminum Coil brings that process to roofing, cladding, and sign stock. Picture a windy coastal job. Salt air. Tight schedule. The installer needs panels that resist creep, keep color, and bend clean. Data says coil lines run 60–200 meters per minute, hit peak metal temperature near 232°C, and can cut field touch-ups by up to 25% (when pretreat and topcoat are matched). But numbers alone do not save a project. They only guide it.
So, what really decides if a façade looks new after five winters? Is it the alloy temper, the PVDF resin load, or the chromate-free pretreat? The truth: it’s the fit between process, environment, and detail work—fasteners, seams, and edge trim. We test with salt-spray hours, gloss retention, and cross-hatch adhesion. Yet the jobsite adds a twist. Bending radius. Tool wear. Heat bounce off dark colors. Small things, big risk. (Yes, very French to care about details.) The question is simple: which contrast in choices matters most when time and weather press hard? Let’s unpack the gaps that hide in plain sight, then move to what’s next.
Part 2: Hidden Pain Points with Trim—Where the Real Fatigue Starts
Where do the quiet failures hide?
painted aluminum trim coil lives at the edges, not the flat field. That is where bends are tight and fasteners bite. Look, it’s simpler than you think. Failures start small: a nick at the slit edge, a sharp bend over 1T, or a mismatched sealant. Traditional fixes rely on heavier gauge or extra caulk. They miss root causes. On a coil-coating line, pretreat chemistry sets adhesion. The PVDF topcoat sets UV and chalk control. But trim needs more: stable gauge tolerance and clean slit edges to avoid micro-cracking. When installers score paint at a 90° fold, the primer has to hold. If the backer coat is too thin, galvanic creep near screws speeds up—funny how that works, right?
Users feel it as callbacks, not lab charts. Drip edges stain. Hemmed corners blister after a hot-cold cycle. Touch-ups never match, and gloss steps show under the eave. Hidden pain points include poor scratch resistance before install, over-baked runs that embrittle, and soft rolls that telescope in transit. A better path starts earlier: specify oven profile by peak metal temperature, verify bend test at 2T with no fissures, and ask for post-slit edge oiling. These are small asks with big effect. They tame handling damage and stop stress cracks at tight bends. The coil still looks sleek, but now it can take abuse. And yes, field crews notice—because the job wraps faster and the punch list shrinks.
Part 3: Forward-Looking Trim—Principles That Make Edges Endure
What’s Next
The next wave is technical and quiet. New pretreats use nano-ceramic films that boost adhesion without heavy metals. IR-enhanced cure ovens cut thermal swing, so the topcoat hits target crosslink with less embrittlement. Spectral color control links the lab to the line; it flags a ΔE drift before a full run goes off-spec. Even better, digital recipes tie gloss, bake curve, and line speed in one loop. Outcome: tighter bend radii with no craze lines, higher abrasion resistance in handling, and steadier color across batches of aluminum trim coil colors. Edges see the worst stress. These principles move strength where it’s needed most—right at the hem and notch.
From our earlier contrasts, we learned that trim fails at edges, not on the big flats; that process fit beats brute thickness; and that field handling can undo good chemistry. Here is how to choose better, in measurable terms. Advisory close. One, bend integrity: demand 2T–3T pass with zero micro-crack under 10× magnification, and cross-hatch adhesion at 5B. Two, weather spine: require QUV-B data with gloss retention above 70% at 2,000 hours and chalk ≤8 on ASTM D4214 for darker aluminum trim coil colors—because dark shades heat up. Three, edge resilience: specify slit-edge quality class, oiling level, and film hardness (pencil hardness HB–H) to protect bends and fasteners. Do this, and you cut rework, stabilize color, and keep hems clean. Not magic—just better alignment of chemistry, cure, and handling. Small moves, large gains—funny how that repeats. Learn, adjust, and keep building forward with yaret.