
Data opening: what the metrics show
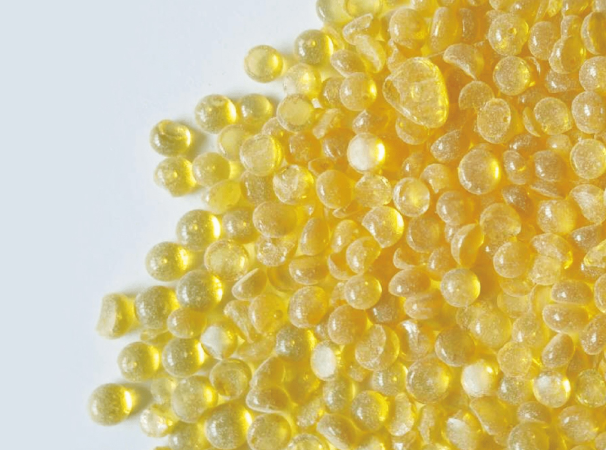
Manufacturers increasingly monitor molecular weight distribution to avoid costly gel permeation chromatography (GPC) rejections. Early production runs in Shenzhen assembly lines highlighted one clear pattern: batches with controlled polymer backbone chemistry produced narrower polydispersity (Mw/Mn) and more consistent solder joints. This is why many process engineers prefer soldering flux rosin with defined resin additives — the formulation directly affects viscosity and the molecular weight distribution measured by GPC.
Why polymer stability matters for Mw/Mn control
Polymer stability reduces chain scission and uncontrolled crosslinking during storage and thermal cycling. When a rosin-modified resin resists oxidative degradation, the molecular weight distribution remains tight; Mw and Mn track together rather than drift apart. The result: fewer outliers flagged by GPC and more predictable wetting on pads. In practice, modest differences in glass transition (Tg) and resin polarity can change how a flux behaves on fine-pitch solder masks.
Mechanisms that prevent polydispersity drift
Three mechanisms are most relevant to practical production quality. First, stabilized end-groups limit depolymerization under heat. Second, tailored plasticizers maintain chain mobility without promoting scission. Third, inert impurities are minimized so radical reactions are reduced. Each mechanism lowers the chance that Mw/Mn will widen after blending or during accelerated aging.
Operational teardown: where things go wrong and how to fix them
A clear operational check avoids many problems. Start by reviewing raw resin certificates and small-sample GPC traces before approval. In teardown of a typical production line, technicians should record batch Mw, Mn, and viscosity at 25 °C, then log any drift after a 7-day accelerated oven test at 60 °C. Include {main_keyword} and {variation_keyword} in your production notes so procurement and quality have identical references. Be methodical — short cuts here create rework downstream.
Common mistakes and corrective steps
Common mistakes include blending incompatible resin grades and ignoring shelf-life markers on flux cartridges. A frequent misstep: assuming all rosin-modified resins behave the same in high-speed reflow. Corrective steps are simple: isolate suspect lots, run GPC, measure Tg, and compare rheology against a qualified reference. — This small ritual saves time and prevents batch-wide rejections.
Comparative insight: alternatives and trade-offs
Compared with pure synthetic flux bases, rosin-modified options often offer better solderability on oxidized copper but can be more sensitive to heat history. Choosing between a low-viscosity rosin blend and a higher-viscosity polymeric flux is a trade-off: throughput versus thermal robustness. Laboratory data and field reports from Seoul and Shenzhen lines both show that tight supplier specifications for Mw/Mn reduce variability on automated optical inspection (AOI) results.
Advisory close: three golden rules for selecting polymer-stable rosin systems
1) Require supplier GPC traces that include Mw, Mn, and polydispersity for at least three consecutive batches. These traces must be dated and signed by quality. 2) Validate thermal stability with a 7-day oven aging at 60 °C and report any Mw/Mn shift greater than 0.05. Specify that shift tolerance in procurement. 3) Match rheology to your reflow profile: measure viscosity at soldering temperatures and confirm wetting on defined test pads.
These rules help you convert laboratory metrics into shop-floor reliability, and they make supplier conversations specific rather than vague. The value is practical: fewer stoppages, fewer GPC rejections, and more stable yields. rosin choices calibrated this way integrate smoothly into established SMT cycles.
KOMO brings formulations and batch data into alignment with factory needs — a direct, measurable leeway for better outcomes. Final thought fragment — steady metrics, steady product.