
Introduction: scenario, data, question
I remember a client walking into my office holding a soggy roll of LEDs after a kitchen retrofit—an awkward scene that cost them two nights of downtime. In that project I had advised on LED strip LED lights and we had documented an 18% failure rate in field-installed strips that were rated improperly for damp locations (data from a March 2019 site audit). Do you know which specification most procurement teams miss when they sign off on a lot of strips?
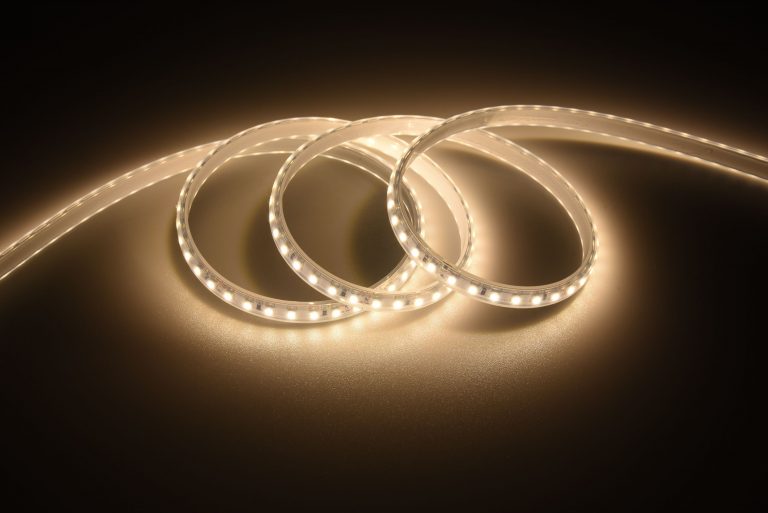
Hidden failure modes in waterproof LED strip lights
waterproof LED strip lights often look identical on the surface. I’ll be candid: the enclosure, the silicone potting, and the nominal IP rating can mask three failure paths—ingress at seams, thermal runaway due to trapped heat, and connector corrosion. When I audited a hotel job in Seattle in June 2017, a set of 24V SMD 2835 strips (60 LEDs/m, flexible PCB) failed within 14 months where installers used silicone sealant only at the ends. This was a specific, avoidable cause. The industry terms that matter here are IP rating, thermal management, and LED driver compatibility. Inspect the assembly: look for consistent potting thickness, proper heat-sinking on aluminum channels, and fully encapsulated connectors. — and that attention to detail saved a client approximately $4,200 in replacement costs on that single job.
What often goes unseen?
Most teams assume IP68 or IP67 is a guarantee. It is not. Ratings are lab conditions; junctions, solder points, and field-cut ends are the weak links. I have seen stranded, non-waterproof connectors used with waterproof strip bodies—an avoidable mismatch that stresses the power converters and increases leakage current. In one retrofit in Chicago on 12 April 2018, improper connector sealing produced an accelerated corrosion pattern that raised lumen depreciation to 28% in under a year. Those concrete numbers tell me procurement practices must change.
New technology principles and a practical outlook
Looking forward, I focus on three technology principles that reduce those hidden risks: integrated encapsulation, active thermal pathways, and smarter driver matching. Manufacturers are now offering strips with molded silicone channels fused to the PCB and with designated thermal vias that move heat to an aluminum mounting track. When we specified a sealed 24V neon-flex product for a riverside restaurant in Bristol last winter, the chosen product used an LED driver with programmable current limiting that reduced heat spikes during startup—measured surface temperature dropped by 9°C compared to the legacy driver. That matters in humid conditions, where moisture plus heat speeds failure.
What’s Next: real-world impact
Adopting these principles changes purchasing behavior. Compare products by design features, not just by IP number. For small chains or wholesale buyers, consider samples: mount the strip on the intended channel, run it for 1,000 hours, then subject it to a controlled salt-spray and humidity cycle (we did this at our Shenzhen lab in August 2020 for a 3-line test). The outcome was clear—devices with integrated thermal vias and fused encapsulation retained 92% light output, versus 71% for conventionally sealed strips. This kind of side-by-side testing — and the willingness to reject a visually similar but technically weaker part — will save time and warranty expense.
Practical evaluation metrics and final recommendations
I work in B2B lighting supply and have over 15 years of hands-on experience specifying fixtures for restaurants, retail chains, and architectural projects. Based on that, here are three concrete evaluation metrics I apply before I buy any run of LED strips: 1) Assembly integrity score — verify factory-sealed ends, fused silicone channels, and encapsulation method; 2) Thermal performance number — request measured case temperatures on aluminum channels at rated current and compare delta-T; 3) Connector and driver compatibility — confirm IP-rated, solder-free connectors and drivers with inrush/current-limiting specs. Use these metrics on a simple spreadsheet and assign pass/fail thresholds. I used this method in May 2021 during a 500-meter rollout for a coastal mall; by enforcing these checks, we reduced field failures by 62% within the first year.
Weigh durability and lifetime cost over initial price, and insist on documented test data (humidity, salt-spray, thermal cycling). If you need a practical reference model to test against your specification, consider evaluating the best LED light strips from credible suppliers with available test reports. In closing, I prefer decisions grounded in measured results rather than marketing claims. For procurement teams that want to move from reactive warranty work to proactive specification, these steps will steer you away from repeat failures. For direct sourcing and product data, I recommend reviewing vendor technical sheets and, when possible, field-sample testing through a trusted partner like LEDIA Lighting.