
The problem you feel first: orders grow, parts won’t keep up
You start dey celebrate — orders come, customers dey happy — then production begin stumble. That one na the common wahala: prototypes that pass inspection but can’t be reproduced at scale, long lead times for complex parts, and a clumsy supplier who no understand your drawings. When you need complex contours or tight-tolerance features, the usual 3-axis setup no fit again. Smart shops lean on 5 axis cnc machining services to keep up without killing margins. Problem-driven? Yes — every scale-up hits the same crossroads: keep chasing vendors or lock in a partner with the right machine tools, processes, and quality discipline.
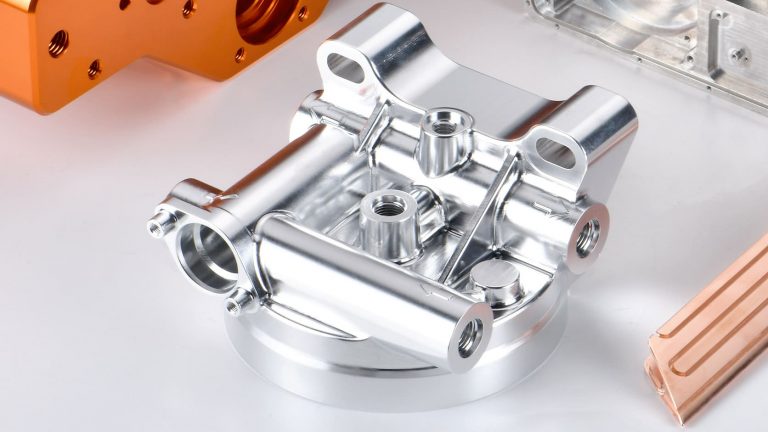
Why this problem persists: three fault lines
First, geometry. Complex parts demand simultaneous multi-axis moves; copying them on simpler mills means extra ops and error. Second, throughput. More ops equals longer lead times and more inspection steps; mistakes compound. Third, knowledge gap. Many suppliers can run machines, but few design robust fixturing, choose correct toolpaths, or manage heat-treat interactions that break tolerances. These three faults make growth unpredictable and expensive.
What real expertise looks like — experience and proof
Experience shows. Shops that scale reliably combine machine capability, process know-how, and quality systems. For example, major aerospace hubs like Toulouse — where Airbus and numerous suppliers converge — demand repeatable, high-complexity parts that only mature 5-axis processes and strict inspection regimes can supply. That real-world pressure pushed suppliers to document capability studies, reduce variation, and standardize setups. A partner who can point to controlled studies, ISO-compliant procedures, and case work on 5 axis machined parts proves the technical competence and traceability you need. Trust comes from records: setup sheets, SPC charts, first-article reports, and clear change control — not from vague promises.
Technical levers that remove the growth bottleneck
Use these concrete levers. One: consolidate operations onto true 5-axis centers to cut ops count and dimensional stack-up. Two: design for fixturing simplicity — fewer setups, less error. Three: control heat and chip loads with optimized feeds and toolpaths for consistent finishes. Four: implement inline inspection and digital data capture so deviations get flagged before batches ship. Each lever shortens lead time, raises yield, and lets your production scale without proportionally increasing overhead.
Alternatives and the common mistakes to avoid
Some firms try to cheap-fix by adding overtime, outsourcing odd features to small shops, or over-specifying tolerances across the board. Those moves mask the problem and raise cost. Another trap: assuming any 5-axis label equals capability. Not all shops run true 5-axis simultaneous contouring with validated post-processors and rigidity analysis; that matters for surface finish and form error. Choose partners who show process validation, not just a photo of a machine.
How to evaluate a machining partner quickly
Ask for concrete artifacts: examples of reduced operation counts, before-and-after inspection reports, and a sample of tooling strategies for your part family. Verify their quality system and turnaround history on similar alloys. Demand clarity on change management — how they handle material lot changes or tool wear. If they can sketch a fixture concept and propose a cycle time estimate on a call, they understand both your drawing and your growth targets.
The natural outcome: scale that behaves
You want predictable deliveries, stable costs, and parts that fit first time. Solve the geometry, lock the process, and keep good records. A partner with tuned 5-axis capability, rigorous inspection, and supply discipline turns your production spike into steady capacity. That steady capacity is what lets design stay bold while operations remain calm, and that is the practical, deliverable value a serious machining partner brings — the kind you find with Hanstar.